
Table of Contents
- Why Legacy Production Tracking Fails Modern Manufacturers
- How to Build a Manufacturing Digital Transformation Roadmap
- Step 1: Assess Your Current Production Tracking Systems
- Step 2: Implement Shop Floor Data Collection Best Practices
- Step 3: Integrate Modern Tracking with Legacy Systems
- When to Choose Custom Manufacturing Software Over Off-the-Shelf
- Calculating ROI and Managing Change on the Factory Floor
- Conclusion
- Frequently Asked Questions
Last Updated: September 21, 2026
Why Legacy Production Tracking Fails Modern Manufacturers
Legacy production tracking fails because it records what already happened, not what is happening now. When job status lives in spreadsheets and paper travelers, the shop floor and front office work from two versions of the truth.
Do not rip out a working ERP to fix a tracking gap. That is the most expensive mistake in this category. Most shops only need the gaps connected, not the core system replaced.
How to Build a Manufacturing Digital Transformation Roadmap
A manufacturing digital transformation roadmap is a phased plan that connects one operational problem at a time to a working fix rather than replacing everything at once. Start narrow and prove value before expanding.
Here is the sequence that works in practice:
- Pick one clearly defined operational problem
- Map how data moves today, including the manual workarounds
- Agree on scope and what “done” looks like
- Deliver a working solution using existing systems where possible
- Measure the result, then move to the next problem
| Phase | Focus | Typical Duration | Success Signal |
|---|---|---|---|
| 1 | One operational problem | Weeks, not months | A working fix in daily use |
| 2 | Connect adjacent systems | Weeks | Data flows without re-entry |
| 3 | Expand and monitor | Ongoing | Fewer manual workarounds |
Step 1: Assess Your Current Production Tracking Systems
Start by listing every place production data gets entered, stored, or moved by hand. Most shops find the same data typed into three places.
Look for these specific signs:
- The same information entered twice or more
- Job status tracked in spreadsheets, not a system
- Quality records stored apart from production data
- Critical steps that depend on one employee’s memory
- Customer paperwork built by hand
Time one job’s full path from order to ship, including every handoff. The minutes you count at each copy point become your ROI story later. Most teams are surprised by the total.
Step 2: Implement Shop Floor Data Collection Best Practices
Shop floor data collection best practices start with capturing data at the point of work, not after the fact, recording what happened while it happens, with as little typing as possible.
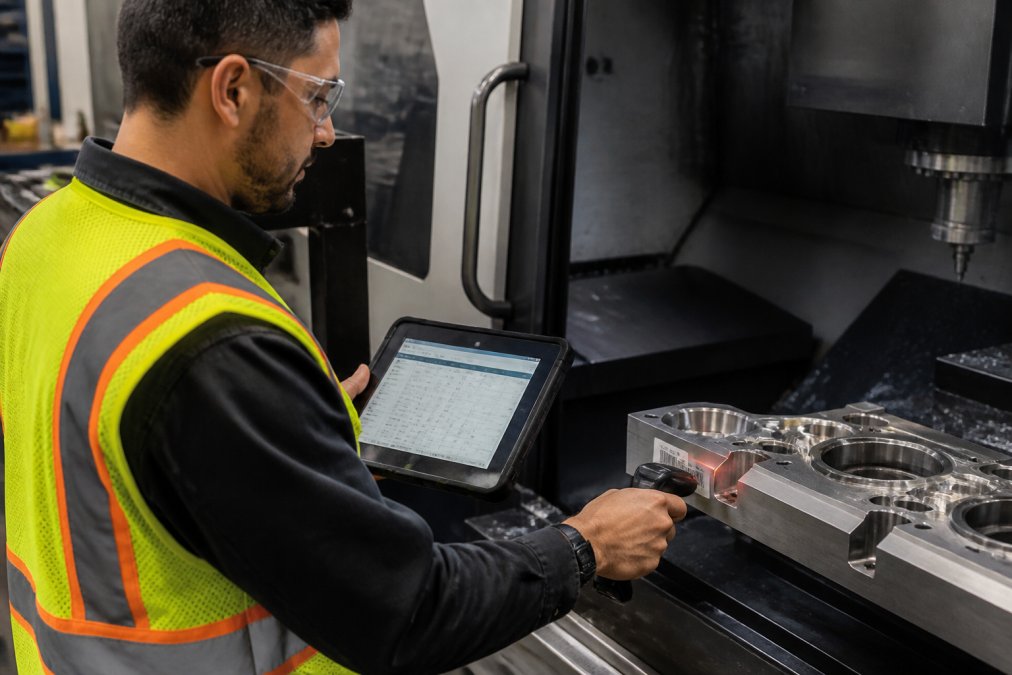
Three rules keep data clean:
- Capture at the source, at the machine or workstation
- Use barcodes, scanners, or machine signals instead of manual entry
- Make the entry step faster than the workaround, or people will skip it
Step 3: Integrate Modern Tracking with Legacy Systems
Integration with legacy systems is where most projects stall, and it does not have to be. The fix is usually a middle layer connecting systems rather than replacing the ERP, MES, or SCADA already running the plant.
- ERP integration keeps orders, inventory, and scheduling in sync
- MES connections tie work orders to actual machine activity
- SCADA links pull real machine states into tracking dashboards
The integration patterns that actually work
There are three patterns, and the right one depends on how old the endpoint is:
- API-first, the ERP or MES exposes a REST or SOAP endpoint, and the middleware polls or subscribes to it. Cleanest option, but many on-premise ERPs only expose a subset of objects this way.
- Database-level, the middleware reads directly from the ERP’s SQL database on a read-only replica or a scheduled query. Fast to stand up, but you must never write back into vendor tables or you void support.
- Machine-level, for older CNC, PLC, and SCADA equipment, you tap the controller directly using OPC UA, MTConnect, or Modbus, then normalize the tags in the middleware before they reach the dashboard.
Before you buy anything, ask each vendor for their integration documentation and a sandbox or test tenant. If they cannot give you either, budget for database-level reads and plan around the support risk.
Cybersecurity for a connected factory floor
Every new connection is a new attack surface, the trade-off nobody puts on the slide, and the reason some IT and OT teams block modernization outright.
A few controls cover most of the risk:
- Network segmentation, keep the OT network (machines, PLCs, SCADA) on a separate VLAN from the corporate IT network. Traffic crosses only through a defined gateway, not by default.
- One-way data flows where possible, a data diode or unidirectional gateway lets machine data flow out to dashboards without letting anything flow back in. For read-only tracking, this removes most of the risk.
- Least-privilege service accounts, the middleware should authenticate with an account that can read the objects it needs and nothing else. No shared admin credentials.
- Encryption in transit, TLS for anything crossing a network boundary, including internal hops between the middleware and the ERP.
- Audit logging, every read and write the middleware performs should be logged, so you can answer “who changed this work order” six months later.
Do not let a middleware vendor open inbound ports to the plant network “just for setup.” That is how a tracking project becomes a security incident. Configure outbound-only connections and revoke temporary access the same day.
Working alongside your existing vendors
This is exactly the kind of gap The Mad Botter fixes: connecting quoting, scheduling, inventory, production, and quality so information stops living in three places at once. We use existing systems wherever practical and work alongside your ERP vendor or MSP rather than replacing them, coordinating with your IT team on segmentation, service accounts, and audit logging so the integration passes review the first time.
The cheapest modernization is almost always integration, not replacement. Connect what works, secure the connections, and fix only what is genuinely broken.
When to Choose Custom Manufacturing Software Over Off-the-Shelf
Custom manufacturing software is right when your process is your edge and no off-the-shelf tool matches how you run. Off-the-shelf wins when your process is standard and speed matters more than fit.
Use this test:
- Choose off-the-shelf if your workflow matches the tool’s defaults closely
- Choose custom if your workflow is a real competitive advantage worth protecting
- Choose custom if you keep bending a standard tool and it keeps breaking
Calculating ROI and Managing Change on the Factory Floor
ROI on production tracking comes from hours saved, errors avoided, and faster job visibility, not the software itself. You prove it by measuring the manual work you remove, the section most guides skip, and the one your CFO and floor supervisor will both ask about.
A ROI framework you can fill in
- Manual data hours per week, count every re-entry, every walk to the floor to check a job, every hand-built report. Multiply by a fully loaded hourly rate (wages plus benefits plus overhead).
- Error and rework cost, scrap, rework, expedited shipping, and credits caused by stale or missing information. Pull this from your quality and accounting records, not from memory.
- Throughput value of faster status, if a job ships a day sooner, what is that worth in freed capacity or earlier invoicing? Even a conservative number here is usually the largest line.
- Fully loaded cost of the fix, software, integration labor, hardware (scanners, tablets, sensors), training time, and ongoing support. Include the internal hours your team will spend, not just the vendor invoice.
The formula is simple:
Annual benefit = (manual hours saved × loaded rate) + (errors avoided × cost per error) + throughput value
Change management: the part that decides whether it sticks
A perfect ROI model does not matter if the floor routes around the new system. Adoption is a people problem, and it follows a predictable pattern.
- Name the floor champions first. Pick the operators and leads who already complain about the current workarounds. Give them early access and let them shape the workflow. They become the people others ask, not the people IT tells.
- Make the new step faster than the old one, or it will not survive. If logging a job takes longer than scribbling on a traveler, the floor will keep scribbling. Design the capture step to be the path of least resistance.
- Train on the job, not in a classroom. A 20-minute session at the workstation, with the operator’s own job on the screen, beats a two-hour slide deck every time.
- Publish the wins. When the first phase removes a manual report or a daily walk, say so out loud. Small visible wins are what buy permission for the next phase.
- Expect a dip. Productivity often drops for the first week or two of any new process. Plan for it, tell leadership it is coming, and do not let it trigger a rollback.
ROI gets the project funded. Change management gets it adopted. Skip either one and the modernization stalls, usually with the software still installed and the spreadsheets still open.
Conclusion
The hardest part of modernizing production tracking is not the technology. It is deciding to fix the gaps instead of living with them.
Frequently Asked Questions
What are the primary signs that a manufacturing production tracking system is obsolete?
Key signs include relying on spreadsheets for job status, entering the same data into multiple systems, chasing paper travelers, and lacking real-time visibility into machine downtime or throughput. If your team spends hours manually compiling shift reports or if critical processes depend on one employee’s knowledge, your production tracking is likely obsolete. These gaps lead to data silos, inaccurate OEE dashboards, and slow decision-making.
How do you integrate modern tracking software with legacy CNC and shop floor equipment?
Integration typically starts with a middleware layer or API that connects legacy equipment to modern databases. For older CNC machines, you may need IoT sensors or data capture hardware to read signals. A phased approach works best: connect one work center, validate data accuracy, then scale. This avoids disrupting production and ensures system interoperability without replacing all legacy systems at once.
What are the most common challenges when upgrading manufacturing data systems?
Common challenges include resistance from shop floor staff, unclear data ownership, and underestimating the effort to clean legacy data. Cybersecurity for connected factory floors is another concern, especially for ITAR-aware manufacturers. A phased implementation roadmap with clear acceptance criteria and change management support reduces these risks. Start with one operational problem, prove ROI, then expand.
How does real-time production tracking impact shop floor efficiency?
Real-time visibility lets supervisors spot bottlenecks immediately, reducing machine downtime and improving throughput optimization. With OEE dashboards updated live, teams can adjust schedules, reallocate resources, and address quality issues before they escalate. Manufacturers often see faster shift handovers and more accurate capacity planning. The result is operational agility and better resource management without adding headcount.