
Table of Contents
- What Shop Floor Integration Actually Requires
- Benefits of ERP and MES Integration for Small Manufacturers
- Challenges of Manufacturing System Integration
- API vs. Middleware vs. Custom Connectors
- How to Connect CNC Machines to ERP
- A Step-by-Step Integration Workflow
- Security, Cybersecurity, and Cost-Benefit Considerations
- Frequently Asked Questions
Last Updated: September 25, 2026
What Shop Floor Integration Actually Requires
Most manufacturers don’t have an ERP problem, they have a gap problem. The ERP handles accounting fine, but the shop floor runs on spreadsheets, whiteboards, and tribal knowledge. Learning how to integrate ERP with shop floor software starts with understanding what you’re connecting.
The Data Layers You Are Connecting
Integration happens across four layers:
- Business layer: ERP handles orders, inventory, purchasing, and financials
- Execution layer: MES or shop floor software manages work orders, routing, and scheduling
- Control layer: PLCs and SCADA systems run machines and collect sensor data
- Physical layer: CNC machines, robots, and sensors generate the raw signals
Data must move between all four. Most failed projects skip a layer or assume the ERP vendor handles it. They don’t.
Benefits of ERP and MES Integration for Small Manufacturers
The benefits of ERP and MES integration come down to one thing: you stop guessing. Job status updates happen automatically when machines run.
Real gains we see in practice:
- Job costing accuracy: Labor and machine time capture at the source, not from memory
- Downtime tracking: Machines report stoppages directly, so you know where hours go
- Inventory accuracy: Material consumption posts to the ERP as work completes
- OEE measurement: Throughput, quality, and availability calculate from real data
Challenges of Manufacturing System Integration
The challenges of manufacturing system integration rarely involve the technology. They involve everything around it.
Three problems show up in almost every project:
- Legacy systems that predate networking: Equipment from the 1990s with serial ports and proprietary protocols
- Data silos between departments: Engineering, production, and accounting each maintain their own version of truth
- Staff resistance to new processes: Operators who’ve tracked jobs on paper for 20 years see no reason to change
Legacy Systems and Data Silos
Legacy equipment often has no API, network port, or documentation, but it still produces parts, so you can’t replace it. The workaround is a gateway device that reads PLC signals or adds sensors to capture machine state.
Change Management for Shop Floor Staff
Operators don’t resist technology, they resist being blamed for problems it creates. A common mistake is rolling out barcode scanning without fixing the underlying process first. If the scan takes longer than a clipboard, adoption dies in a week.
What works:
- Involve operators in design decisions before you build anything
- Start with one work center, not the whole shop
- Make the new process faster than the old one, or don’t bother
- Train on real jobs, not test data
Rolling out shop floor software without operator input is the fastest way to a failed project. If the people running the machines didn’t help design the workflow, they’ll work around it within a month.
API vs. Middleware vs. Custom Connectors
Your connection method determines project cost, timeline, and who you call when it breaks at 2 a.m. Most guides list three options and stop; the useful version explains what each is under the hood, when it wins, and how it fails.
What Each Method Actually Is
Direct API integration means your code calls the ERP’s published endpoints, typically REST over HTTPS with JSON, or SOAP/XML on older systems. The vendor defines the contract; you authenticate (OAuth 2.0 or an API key), send a request, and get a response. No translation layer sits between you and the ERP.
Decision Criteria That Actually Matter
Work through these questions in order:
- Does the ERP expose a documented, supported API? If yes, direct API is usually the cheapest path. If the vendor only supports file drops or a database view, you are building a connector whether you call it that or not.
- How many systems are in scope? One ERP plus one MES is a connector problem. Five systems with overlapping data is a middleware problem.
- How often will the mapping change? If production engineers will want to add fields monthly, middleware’s configuration UI beats redeploying code.
- Who maintains it after go-live? A connector needs an engineer. Middleware needs someone who understands the platform. API calls need someone who can read vendor release notes.
- What is the latency requirement? Real-time job status (seconds) pushes you toward event-driven APIs or MQTT. Batch reporting (hourly or nightly) tolerates file-based approaches.
Trade-offs and Failure Modes
| Method | Best For | Typical Failure Mode |
|---|---|---|
| Direct API | Modern ERP with documented endpoints and stable schemas | Vendor changes a field or deprecates an endpoint; rate limits throttle high-frequency calls |
| Middleware | Connecting many systems with standard protocols | Subscription creep, opaque error handling, and a vendor between you and the fix |
| Custom connectors | Legacy systems, unusual data, tight control needs | Bus factor of one; undocumented code that nobody wants to touch in two years |
A pattern worth naming: hybrid architectures are common and underdiscussed. Many shops run a custom edge connector at the machine (nothing off-the-shelf speaks to a 1998 PLC) plus middleware between MES and ERP (the mapping changes often). You don’t have to pick one method for the whole project.
A Practical Starting Point
For one painful machine and a modern ERP, a custom connector scoped to that machine is the fastest proof of value. For three or more integrations you’re tired of maintaining individually, middleware earns its subscription. Direct API is the default when the vendor supports it and the data model is stable.
Write down who owns the integration after go-live before you pick a method. The method that fits your maintenance capacity beats the method that looks best on a slide.
How to Connect CNC Machines to ERP
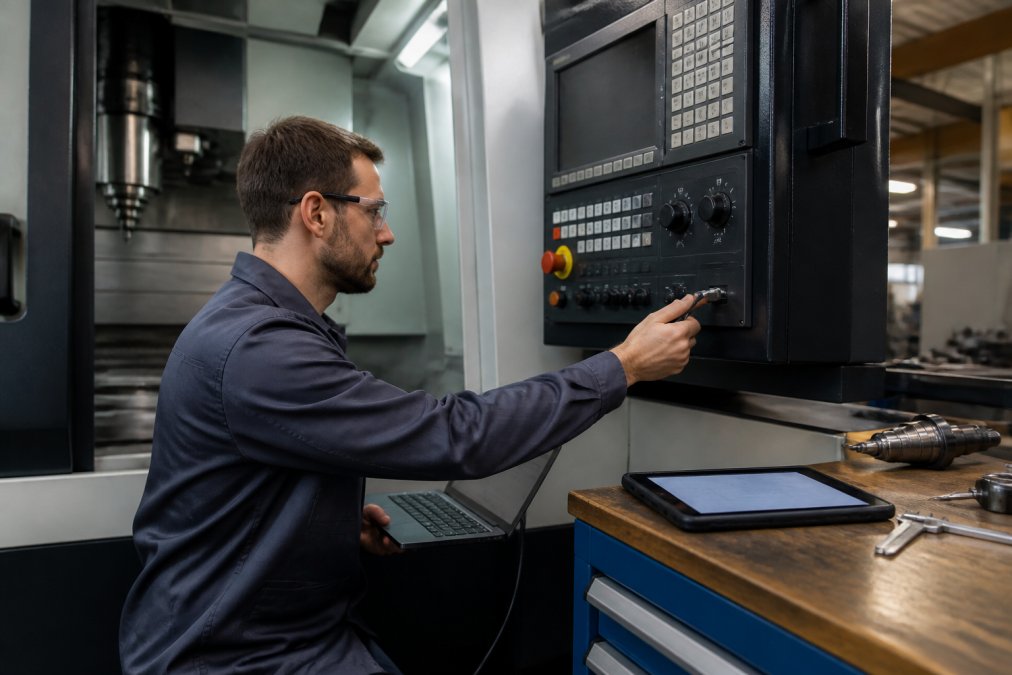
Connecting CNC machines to ERP means extracting machine signals, translating them into job data, and posting that data to the ERP. The machine doesn’t know your work orders; the ERP doesn’t know the spindle is running. You build the bridge.
Mapping Machine Signals and PLC Data
Start by listing the signals you actually need. Not every data point matters.
Common signals worth capturing:
- Cycle start and stop: Tells the ERP when a job begins and ends
- Part count: Confirms quantity produced
- Alarm codes: Flags quality or maintenance issues
- Spindle load: Indicates tool wear or process problems
- Program number: Links the run to a specific work order
A Step-by-Step Integration Workflow
A practical integration follows a defined sequence. Skipping steps creates rework.
- Define the operational problem. Pick one: job status visibility, downtime tracking, or inventory accuracy. Not all three.
- Document current data flow. Walk the floor. Watch how information moves today, including the workarounds.
- Identify systems and signals. List every system involved and the specific data points you need from each.
- Choose your connection method. API, middleware, or custom connector based on your systems.
- Build the data mapping. Match source fields to destination fields with clear rules for edge cases.
- Pilot on one work center. Run the integration on a single machine or process for two to four weeks.
- Measure against baseline. Compare job costing accuracy, data entry time, and error rates to your starting point.
- Expand in phases. Add work centers one at a time. Fix issues before scaling.
The single most important step is defining one operational problem. Projects that try to fix everything at once fail. Projects that fix one thing completely tend to expand successfully.
Security, Cybersecurity, and Cost-Benefit Considerations
Connecting operational technology (OT) to IT is the part most guides skip, and the part that can shut a plant down. Once a shop floor device can write to the ERP, the two networks become one attack surface unless you deliberately separate them.
Why IT/OT Convergence Changes the Risk Model
Traditional IT security assumes you can patch, reboot, and reimage. Shop floor equipment often can’t tolerate any of those without stopping production. A CNC controller on an unsupported OS may be safe on an isolated network and become a liability the moment it can reach the internet or the ERP.
Controls to Put in Place Before You Connect Anything
- Network segmentation. Put shop floor devices on a separate VLAN or, better, a separate physical network with a firewall between it and business systems. Allow only the specific traffic the integration needs, typically outbound from an edge gateway to a known ERP endpoint on a known port.
- A DMZ or data diode pattern. For high-consequence environments, route data through an intermediary host that can read from OT and write to IT but not the reverse. This blocks a compromised ERP from reaching machine controllers.
- Least-privilege service accounts. The integration should authenticate as a dedicated account with permission to write only the specific ERP objects it needs, work order status, quantity complete, downtime events, and nothing else.
- Input validation at the boundary. Never trust data arriving from the shop floor. Validate ranges, reject malformed payloads, and log every rejection. A misconfigured sensor that reports a part count of 999,999 should be caught before it posts.
- Immutable audit logging. Every automated transaction should be logged with timestamp, source, and payload. This is what lets you answer “why did inventory change?” six months later, and it is often a compliance requirement.
- Change control on both sides. An ERP upgrade that changes a field name can silently break the integration. Treat the integration as a system with its own change process.
Regulatory Overlays Worth Knowing
If you supply aerospace or defense primes, ITAR and CMMC reach into your integration design. CMMC expects documented network boundaries, access controls, and audit trails, the same controls that make an integration safer also make it auditable. If you handle controlled unclassified information, confirm with your compliance lead before routing shop floor data across a shared network.
A Cost-Benefit Framework You Can Actually Run
- Labor hours recovered. Count the people who currently enter or reconcile production data, and how many hours per week they spend on it. Multiply by a fully loaded hourly rate.
- Error cost. Estimate the frequency of data errors (wrong quantities, missed job completions, mis-posted material) and the average cost to correct each one, rework, expedited shipping, credit memos, customer escalations.
- Throughput and OEE gains. If real-time downtime data lets you recover even a small percentage of machine availability, that flows directly to revenue. Be conservative here; this is the number most likely to be overstated.
- Total cost of ownership. Include build or license cost, integration platform fees, the engineering time to maintain it, and the cost of the security controls above. Ongoing cost usually exceeds build cost within two to three years.
The most common cost mistake is budgeting for the build and not for the maintenance. Integrations break when ERPs update, when machines are replaced, and when the one engineer who built it leaves. Budget for ownership, not just delivery.
If your team lacks the engineering capacity to design the security boundary and maintain the connection, that is where a partner like The Mad Botter comes in. We start with one defined problem, agree on scope, and deliver a working solution using your existing systems. No army of junior consultants. Senior engineers only.
Frequently Asked Questions
What is the difference between MES and ERP integration?
ERP manages business functions like quoting, purchasing, job costing, and inventory. MES controls and tracks what happens on the shop floor in real time, including work orders, machine status, and quality checks. Integration means the two systems share data automatically: the ERP sends the work order down, and the MES sends completion, scrap, and labor data back up. Without integration, someone re-enters that data by hand, which introduces errors and delays job costing accuracy.
What are the primary benefits of real-time data integration between ERP and the shop floor?
Real-time shop floor integration gives you production visibility without chasing paper travelers or calling the floor for status. Job costing updates as work completes instead of days later. Inventory accuracy improves because material consumption posts when it happens. Downtime tracking and OEE data flow into reports automatically. For a 40-person shop, the biggest gain is usually eliminating double entry and the spreadsheet workarounds that hide problems until month-end.
How do you handle legacy machine data during an ERP integration?
Start by inventorying what each machine can output. Older CNC machines may only have serial or digital I/O, while newer ones support MTConnect or OPC UA. For machines with no network capability, you add sensors or a data collection device at the control. Then map each signal to a meaningful event in your ERP or MES, such as cycle start, cycle end, or fault code. Test with one machine before rolling out to the rest of the floor.
What are the common challenges when connecting PLC data to ERP systems?
The main challenges are data mapping, timing, and ownership. PLCs speak in tags and registers, while ERP expects job numbers, quantities, and cost codes. Someone has to define that translation and keep it accurate when processes change. Network segmentation matters too: your PLC network should not sit flat against your business network. Finally, decide who owns the integration long-term, because a connector that nobody maintains becomes another data silo within a year.